Pyrocraft Technologies industrial waste heat recovery plant with chimneys venting exhaust heat
Factory Exhaust Recovery

Capturing Lost Flue Gas

Reclaiming thermal energy from high-temperature manufacturing chimneys.

PYROCRAFT TECHNOLOGIES PRIVATE LIMITED — COIMBATORE

Turning wasted factory heat into savings.

Industrial waste heat recovery for Indian manufacturers. We audit where heat is lost, recover it with heat exchangers, and prove the fuel saved every month — with no change to your core process.

Start Saving Fuel

Assess your plant's potential waste heat recovery with our on-site measurement survey.

Our Systematic Approach
1 Measure
→
2 Recover
→
3 Reuse
→
4 Prove

"Flue gas often leaves at 200–400°C — and that energy is lost."

Industrial thermal energy recovery and manufacturing plant infrastructure

Illustrative imagery — real site photos to be added.

The Industrial Challenge

Factories burn expensive fuel and then vent the heat.

Thermal processes consume significant capital, yet huge quantities of usable energy escape through stacks and exhausts daily.
Industrial thermal exhaust venting from boiler chimney

Heat is thrown away every day

Boilers, furnaces, thermal oil heaters, dryers, ovens and diesel generator sets release hot exhaust. Flue gas often leaves the chimney at 200–400°C, and all that energy is lost.

High-voltage industrial energy infrastructure and electrical power transmission grid

Energy is a major cost

Fuel (coal, diesel, furnace oil, gas) and power make up a large part of running cost for textile, foundry, food and engineering units, and fuel prices are unpredictable.
MSME industrial manufacturing plant floor

MSMEs are left behind

Large plants hire consultants for heat recovery, but small and mid-size units rarely do. They lack in-house thermal engineers, spare capital, and trust in unproven vendors.

Industrial emission reporting and sustainability compliance

Pressure is growing

Export buyers increasingly ask suppliers to cut energy use and report carbon emissions.
The gap: a local, affordable partner who can audit, design, install and prove the savings.
Explore Our Services
Boiler room with heavy industrial pipes and high pressure vessels

Bridging Thermal Efficiency & Factory Operations

Standardizing waste heat recovery across Indian manufacturing boilers, furnaces, and heaters.

Illustrative imagery — real site photos to be added.
Our Methodology

We capture exhaust heat and put it back to work.

A non-invasive, turnkey cycle engineered specifically for operational stability and transparent verification.

Engineers in a workshop conducting thermal measurements
Step 1 — Baseline Survey

Measure

Audit where heat is lost, recording exhaust temperature, flow rate, fuel use and operating hours.

Industrial thermal heat recovery exchanger fitting
Step 2 — Heat Exchangers

Recover

Fit heat exchangers (economizers, air preheaters, hot water units) that pull heat out of exhaust before it leaves.

High pressure process hot water and steam piping
Step 3 — Process Integration

Reuse

The recovered heat becomes boiler feed water, preheated combustion air, process hot water or space heating.
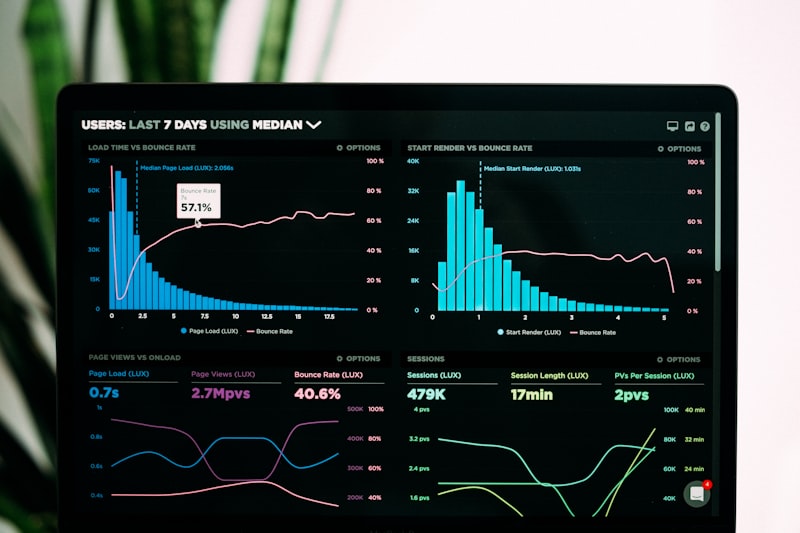
Digital dashboard displaying fuel savings metrics
Step 4 — Continuous Verification

Prove

Sensors and a dashboard show the fuel saved each month, so the customer sees the return.

⚙️
Lower fuel bills with no change to the core process
📈
Faster payback than most machinery investments
🌱
Lower emissions as a side benefit
💡

"A commonly cited figure is about 1% fuel saving for every 20–22°C drop in boiler flue gas temperature. Actual savings are confirmed per site during the audit."

Our Offerings

End-to-End Waste Heat Solutions

From initial site thermal diagnostic surveys to rugged custom equipment and continuous telemetry.
Safety inspection engineer wearing safety glasses conducting audit

Heat Audit

Site survey and measurement of all waste heat sources; report with estimated savings, system design and payback period. Entry service that builds trust.

Economizer unit with finned heat exchanger tubes

Economizers and Air Preheaters

Recover flue gas heat into boiler feed water or combustion air; suited to boilers, furnaces and thermal oil heaters.
Industrial plant warehouse with process water machinery

Waste-Heat Hot Water Units

Convert exhaust heat from compressors, DG sets and ovens into process hot water; suited to textile processing, dairy and food units that need constant hot water.
Code screen showing developer dashboard work

Savings Monitoring

IoT sensors, a cloud dashboard and monthly savings reports; alerts on fouling, leaks and efficiency drops. Sold as a subscription, attached to every installation.

Project Execution

How We Deliver Your System

A structured engineering process from initial baseline measurement to live telemetry.
Engineer inspecting facility with digital tablet
Step 1 1–2 weeks

Audit

Site survey and measurement.

Engineering thermal calculations and blueprints
Step 2 2–3 weeks

Design

System design and payback estimate.
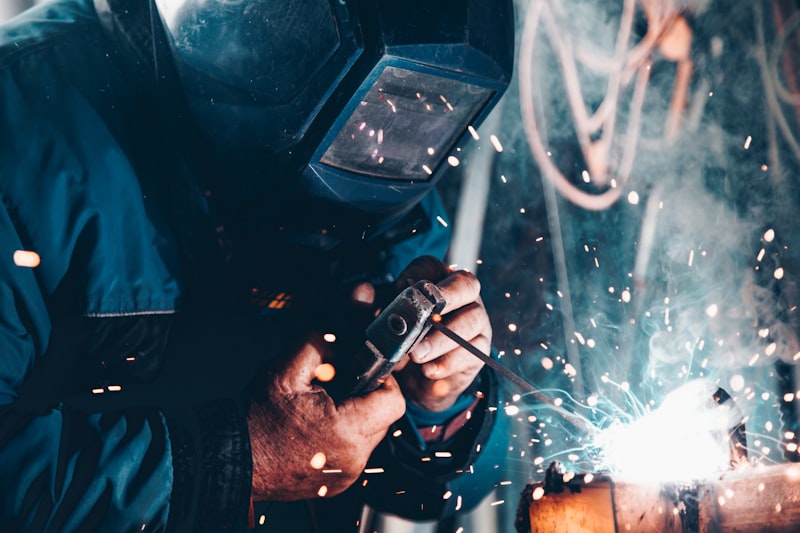
Pipe installation welding with sparks
Step 3 2–6 weeks

Install

Installation by certified local fabrication partners.
Engineers conducting reports review and analytics
Step 4 Ongoing

Track

Sensors, dashboard and monthly savings reports.

Timings are typical ranges; the exact schedule is confirmed per site after the audit.

Industrial manufacturing furnace glow and radiant heat recovery

High-Heat Industrial Energy Reclaimed

Transforming radiant exhaust energy into practical boiler feed water and hot process circuits.

Illustrative imagery — real site photos to be added.
Engineering Architecture

Proven thermal engineering plus modern monitoring.

Combining robust mechanical heat exchange with connected telemetry for verified performance.
🔩

Thermal Hardware

Shell-and-tube, plate and finned-tube heat exchangers; materials chosen per application, such as stainless steel or corrosion-resistant alloys where flue gas can condense.

📡

IoT and Controls

Thermocouples, flow meters and pressure sensors; PLC-based controls and bypass dampers to protect equipment; data sent over mobile networks or Wi-Fi.

💻

Software

Cloud dashboard with live temperatures and fuel-saved calculations; analytics for savings forecasts and early warnings of fouling or faults. Built and maintained by our developer, [email protected].

🧠
PLANNED, NOT YET BUILT

AI components — PLANNED

Fouling / fault anomaly detection (planned): flag efficiency drops from exhaust temperature, flow rate, fuel use and operating hours. Model family proposed, to be confirmed: autoencoder or Isolation Forest, trained from scratch on collected sensor history.

Fuel-savings forecasting (planned): forecast fuel saved per site from the same sensor history plus fuel consumption and the audited baseline. Model family proposed, to be confirmed: gradient-boosted trees, trained from scratch on collected sensor history.

⚡
PLANNED, NOT YET BUILT

Where NVIDIA fits — PLANNED

  • Training on collected sensor history → CUDA (planned, could fit)
  • Production inference for alerts and forecasts → TensorRT (planned, could fit)
  • Serving multiple site models from the dashboard backend → Triton Inference Server (planned, only if backend serving is used)
  • On-site inference at a plant with no reliable cloud link → Jetson (planned, optional, only if on-site deployment is chosen)
"Removing the planned ML leaves the current hardware + dashboard product working. The ML is an addition, not yet the core."
Heavy heat exchanger installed beside an industrial furnace
Mechanical Reliability

Corrosion-Resistant Exchanger Assemblies

Each unit features tailored tube metallurgy and automated safety bypass dampers to safeguard your boiler draft and furnace pressure under all operational conditions.

"Why this matters: the hardware is proven technology, so the technical risk is low — and the monitoring layer is what makes us different from a plain fabricator."
Sector Applications

Industries We Serve

Engineered for energy-intensive manufacturing clusters in Tamil Nadu and across India.

Industrial textile manufacturing machinery and automated looms

Textile

Recovering boiler exhaust for stenter heating, washing baths, and dyeing water circuits.

Molten metal casting and fiery foundry pouring with sparks

Foundry

Capturing furnace flue gas to preheat combustion air and charge materials.

Stainless steel sanitary dairy tanks and process pipelines

Food and Dairy

Converting boiler & compressor heat into constant sanitary process hot water.

Engineering fabrication workshop with heavy machinery

Engineering & Fabrication

Harnessing heat from curing ovens, thermal fluid heaters, and heat treatment lines.

Commercial Flexibility

How We Work With You

Flexible engagement models designed to align with your capital allocation and energy reduction targets.

Industrial plant construction site

Project Sales

One-time supply and installation of a heat recovery system, scoped per site.
Contact for Pricing
Professional business handshake representing partnership

Savings Sharing

A share of measured fuel savings over an agreed term, structured around audited baseline performance.
Contact for Pricing
Industrial service and maintenance verification sign

Dashboard Subscription

Monthly monitoring, reports and alerts.

Contact for Pricing
Boiler system ongoing preventative maintenance

Annual Maintenance (AMC)

Yearly maintenance and support.

Contact for Pricing
Industrial factory and refinery illuminated at night with lights

Continuous Industrial Energy Efficiency

Around-the-clock savings verification for high-uptime manufacturing lines.

Illustrative imagery — real site photos to be added.
Clear Answers

Frequently Asked Questions

Facts regarding system operation, installation timelines, and verified returns.

Q. What is waste heat recovery?

Capturing exhaust heat that would otherwise leave through the chimney and reusing it for feed water, combustion air, hot water or heating.

Q. Will it change our core process?

No — the system sits on the exhaust side; your core process is unchanged.

Q. How long does a project take?

Typically 1–2 weeks for audit, 2–3 weeks for design, 2–6 weeks for installation, confirmed per site.

Q. How are savings proven?

Sensors and a dashboard show the fuel saved each month; actual savings are confirmed per site during the audit.

Q. Do you serve small factories?

Yes — MSMEs are a core focus; the heat audit is the entry service.

Q. What routine maintenance is needed?

Our heat recovery systems are engineered for high uptime with automated bypass dampers and IoT fouling alerts, requiring only periodic scheduled inspections.

Leadership

The team behind Pyrocraft

Focused on industrial thermal efficiency, project execution, and telemetry monitoring.

ASR

Anush Shyam Ravikumar

Director

Strategy, customer relationships, partnerships

KD

Keval Das

Director

Operations, finance, project delivery

AG

Amit Gohil

Developer

Monitoring platform and dashboards

Factory with chimneys at night

Let's cut your fuel bill together.

Schedule a comprehensive site waste heat survey. We identify recoverable thermal energy, model monthly rupee savings, and prove your payback.

Book a Free Heat Audit

Request a Heat Audit

Submit your plant details below. This form directly generates an email to our Director, Anush Shyam Ravikumar.

🔒 Direct client trigger: opens your default email client addressed to [email protected] with no third-party tracking.

Company Headquarters

📍
Registered Address
No. 496, B3, CAG Central, Avinashi Road,
Coimbatore South, Coimbatore,
Tamil Nadu 641004, India
📞
Phone
✉️
Primary Email
Corporate Identity Number (CIN)
U28199TZ2024PTC030985
Incorporated 18 March 2024

Company details as provided.